How to Choose CBN Cutting Tools for Global Sourcing?
Choosing Cbn Cutting Tools for global sourcing requires more than comparing prices or catalog images. The right selection depends on workpiece material, hardness, machine stability, cutting speed, and expected tool life. A tool that performs well on hardened steel may fail on cast iron or powder metallurgy parts. Small differences matter. A rigid setup, balanced holder, and controlled coolant supply can strongly influence the final result.
Experienced buyers usually begin with the cutting application, not the supplier’s sales claims. Ask for grade specifications, recommended cutting parameters, coating details, inspection records, and sample-testing support. Reliable manufacturers should explain how their CBN content, binder system, and edge preparation suit your operation. They should also provide consistent batch documentation, clear packaging information, and responsive technical assistance across time zones. Independent certifications can support trust, but they should never replace practical testing.
Global sourcing also introduces risks that are easy to overlook. Shipping conditions, replacement lead times, communication gaps, and changing quality between batches can affect production. A short trial on an actual machine may reveal more than a polished brochure. No sourcing plan is flawless. Even experienced teams can choose an unsuitable edge geometry after focusing too heavily on unit cost. Careful records help correct that mistake. By comparing measurable results, supplier transparency, and long-term support, manufacturers can select Cbn Cutting Tools with greater confidence and fewer unexpected interruptions.
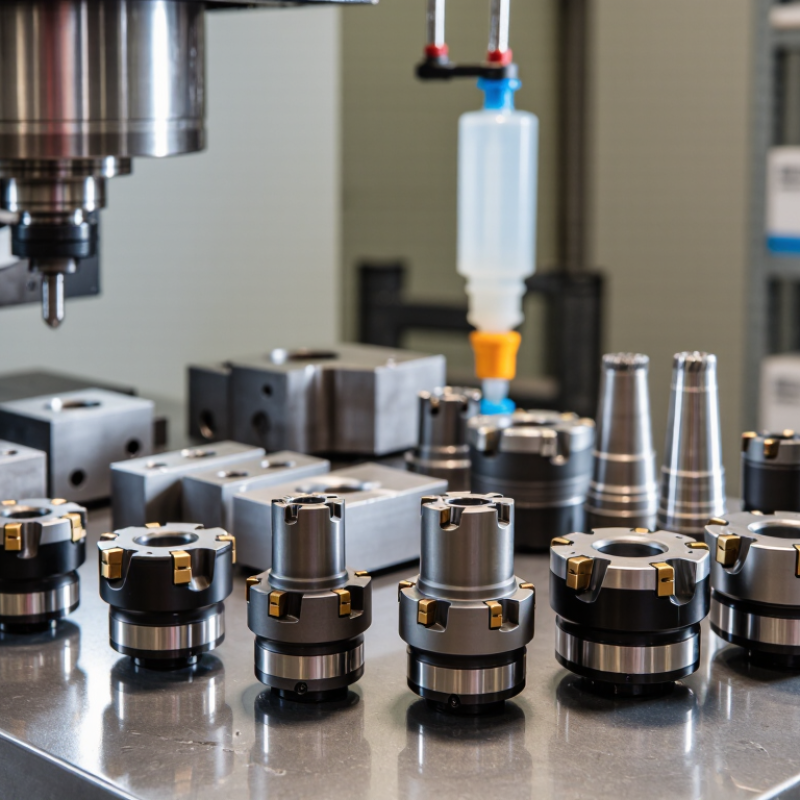
Define CBN Cutting Tools and Their Key Advantages
Cubic boron nitride, or CBN, is a synthetic superhard cutting material. It is designed mainly for machining hardened steels, cast irons, powder metals, and other difficult ferrous alloys. Unlike diamond tools, CBN usually performs better when cutting iron-based materials at elevated temperatures. Its hardness helps the cutting edge resist abrasion during demanding production work.
The key advantage is stable wear resistance. A properly selected CBN insert can maintain its edge while producing consistent dimensions and surface finishes. This matters when turning hardened shafts, bearing races, or automotive components. CBN also supports high-speed machining and may reduce grinding operations.
However, it is not a universal solution. Not always.
Tool performance depends on the CBN content, binder type, edge preparation, workpiece hardness, cutting speed, and coolant strategy. A high-CBN grade may suit interrupted cuts, while a lower-content grade can deliver better finishing performance. In sourcing trials, compare actual tool life, chip control, edge damage, and finished roughness rather than relying only on catalog claims. That distinction matters.
Global buyers should request material specifications, dimensional tolerances, inspection records, and batch consistency data. Clear technical communication prevents costly mismatches between the insert and machine conditions. A small edge defect can become visible as vibration, burrs, or uneven wear. CBN tools cost more initially, but predictable performance can justify the investment when the application is correctly matched. Mistakes still happen, especially when test conditions do not reflect factory production.
Match CBN Grades to Workpiece Materials and Cutting Conditions
CBN grade selection starts with the workpiece, not the catalog title. Hardened steel, cast iron, and nickel-based alloys need different edge behavior. For hardened steel above 45 HRC, a lower-CBN-content grade with a ceramic binder often gives a sharper finishing edge. Heavy interrupted cuts need stronger support and higher CBN concentration. Cast iron usually rewards a tougher grade that tolerates abrasive dust and vibration.
Market data supports careful qualification. MarketsandMarkets estimated the global superabrasives market at about USD 7 billion in 2024, with automotive and aerospace among major users. The U.S. Geological Survey’s Mineral Commodity Summaries 2024 also highlights continued demand for advanced cutting and grinding materials in high-performance manufacturing. These figures show market growth, but they do not replace testing. Cutting speed, feed, depth of cut, coolant, and workholding can change tool life quickly. A grade that performs well on stable steel may fail during a 0.3 mm interrupted cut. That detail is often underestimated.
Tips: Match grade, binder, and edge geometry together. Start with conservative speed and feed. Inspect flank wear after a short run. Reduce speed before changing the grade. A practical trial cut can reveal more than a polished specification sheet. I have seen operators blame the CBN grade when vibration caused the real failure. That assumption deserves review. Also check whether coolant delivery is consistent, especially near corners and interrupted surfaces.
Evaluate Tool Geometry, Coatings, and Performance Requirements
When sourcing CBN cutting tools globally, geometry should match the workpiece, not the catalog image. Rake angle, clearance angle, edge preparation, and nose radius control cutting force and chip flow. For hardened steel, a stable edge often matters more than an aggressive rake. A small chamfer can resist chipping during interrupted cuts. Measure twice. I once selected a sharp edge for a difficult batch, and vibration damaged the finish within minutes. That mistake changed my approval process. I now request cutting data, drawings, and sample results before comparing prices.
Coating selection should follow heat, friction, and material behavior. A multilayer coating may reduce wear during continuous turning. An uncoated or differently engineered surface may perform better in abrasive applications. Confirm coating thickness, adhesion testing, and operating temperature limits with the supplier. Ask for evidence from comparable hardness and cutting speeds. “Premium” is not a performance specification. It still matters. Inspect the edge under magnification. Uneven coverage can reveal handling or process problems.
Performance requirements need measurable limits. Define tool life, surface roughness, dimensional tolerance, spindle load, and acceptable chipping before ordering. Include coolant conditions, workholding, machine rigidity, and insert change procedures. These details affect results as much as tool material. Run a controlled trial with identical feeds and speeds. Record wear at fixed intervals. A supplier should provide traceable inspection records and consistent batch identification. Global sourcing adds transport and communication risks, so approve a backup specification, not just a backup vendor. Even careful trials can mislead when the operator changes mid-test. Review the data honestly.
Verify Supplier Quality, Certifications, and Global Compliance
When sourcing CBN cutting tools globally, supplier claims should become documented checks. Product photos are not enough. Ask for material certificates, dimensional inspection reports, and batch traceability records. These documents should identify the CBN grade, cutting geometry, substrate, coating, and inspection date. Small details matter.
Review the supplier’s quality system before discussing price. An ISO 9001 certificate can indicate controlled processes, but it does not guarantee consistent tool performance. Confirm the certificate’s validity, issuing body, covered site, and scope. Request samples from recent production batches. Measure edge preparation, insert thickness, and tolerance with calibrated equipment. Ask how rejected tools are isolated and recorded. A clear nonconformance process often reveals more than polished sales language.
Global compliance requires destination-specific attention. Check product classification, packaging rules, chemical declarations, and required export documents with qualified trade professionals. Requirements can differ between regions and may change. Do not accept a generic compliance statement. Request signed declarations and retain revision-controlled records. Supplier audits should also examine worker safety, environmental controls, and subcontractor management. These areas affect continuity and reliability, even when the tool itself meets specification.
I once treated certification as proof of quality. That was too simple. A valid certificate cannot replace cutting tests, traceability, or honest communication about process limits. Ask the supplier to explain tool life results using your workpiece material, machine condition, coolant method, and cutting parameters. If the answer stays vague, pause the order. Performance evidence beats confident wording.
How to Choose CBN Cutting Tools for Global Sourcing?
A practical supplier-verification model for CBN cutting tools. The priority scores reflect the relative importance of quality evidence, product traceability, certification review, and destination-market compliance during global sourcing.
Verify certificate scope and validity with the issuing body. ISO 9001 supports quality-system verification, while REACH and RoHS obligations depend on the destination market, product composition, and application. Treat the scores as a sourcing framework rather than a substitute for legal or technical review.
Compare Total Costs, Logistics, and Long-Term Supply Reliability
When sourcing CBN cutting tools globally, the lowest quoted price rarely represents the lowest usable cost. A practical comparison includes tool price, coating options, freight, customs handling, inspection, and replacement time. Record consumption by machine, workpiece material, cutting speed, and failure mode. A tool that lasts 30% longer may still lose value if delivery takes six weeks. This happens.
Ask suppliers for consistent technical data, sample measurements, packing standards, and documented lead-time history. Request pilot quantities before committing to annual volume. During trials, track edge wear, surface finish, cycle time, and unexpected stoppages. One overlooked delay can cost more than several premium tools. Use landed cost per finished part, not price per insert. However, calculations can mislead when production conditions change. Our team once compared suppliers using stable batch data, then faced inconsistent hardness in later material. A supplier’s quality record matters, but it does not replace incoming inspection.
Long-term reliability depends on capacity, backup processes, communication, and realistic safety stock. Confirm whether critical grades have alternative production routes and whether technical drawings remain controlled. Keep a small buffer near the plant when downtime costs are severe. Yet excessive inventory ties up cash and can hide weak forecasting. Review performance quarterly, and challenge assumptions when results look unusually good. The uncomfortable question is simple: can this source recover after a missed shipment?
How to Choose CBN Cutting Tools for Global Sourcing? — Compare Total Costs, Logistics, and Long-Term Supply Reliability
Anonymized planning benchmark for standard CBN insert sourcing, based on a requirement of 3,000 usable cutting edges per year.
| Sourcing Route |
Quoted Price
per Insert |
Usable Edges
per Insert |
Typical Defect
or Rework Rate |
Freight and
Insurance |
Import Duty
Allowance |
Order-to-Delivery
Lead Time |
Minimum Order
Quantity |
Estimated Landed Cost
per Usable Edge |
Annual Cost for
3,000 Usable Edges |
On-Time Delivery
Rate |
Long-Term Supply
Risk |
Regional inventory
with domestic replenishment |
$42.00 |
2.5 |
1.5% |
$4.00 |
0% |
5–10 calendar days |
20 inserts |
$19.55 |
$58,650 |
96% |
Low |
Consolidated ocean freight
with scheduled releases |
$28.00 |
2.5 |
2.0% |
$1.80 |
8% |
35–55 calendar days |
100 inserts |
$14.08 |
$42,240 |
91% |
Medium |
Air freight for urgent
or low-volume orders |
$31.00 |
2.5 |
2.0% |
$8.00 |
8% |
7–14 calendar days |
50 inserts |
$17.84 |
$53,520 |
94% |
Low to Medium |
Single-source offshore
direct purchase |
$25.00 |
2.5 |
3.5% |
$1.50 |
8% |
45–70 calendar days |
200 inserts |
$13.99 |
$41,970 |
84% |
High |
Dual-source strategy:
70% ocean and 30% regional |
$32.20
weighted average |
2.5 |
1.8% |
$2.46 |
5.6% |
15–45 calendar days |
80 inserts
combined |
$15.72 |
$47,160 |
95% |
Low |
Cost basis: Estimated landed cost per usable edge includes quoted insert price, freight, insurance, import duty allowance, inbound handling, normal quality loss, and inventory carrying cost during transit. Annual cost excludes machine downtime, tooling changeover labor, taxes recoverable by the buyer, and currency-hedging costs.
Selection guidance: Consolidated ocean freight generally provides the lowest planned cost at stable demand volumes. A dual-source model offers a stronger balance between cost, delivery performance, and continuity for critical production lines. Actual results should be validated against the destination country’s tariff classification, freight quotation, quality records, and contractual lead-time commitments.
 Skip to content

 English
 Russian
 German
 Spanish
 French
 Portuguese