...

How to Choose the Right Exothermic Welding Powder?

Choosing the right Exothermic Welding Powder is about matching the material to the connection, not simply picking a familiar product. The correct choice depends on conductor metals, cable or rod dimensions, connection design, and the mold specified for the job. A powder used successfully on one setup may not suit another. Small differences matter.

Begin by checking the connector and mold specifications. Record the conductor type and size, then compare them with the powder manufacturer’s product information. Look for a clearly stated application and charge size. An incorrect match can produce a weak or inconsistent connection, even when the setup appears sound. That detail is easy to overlook.

Supplier guidance is useful, but it should not replace the product instructions. Confirm that the powder, mold, and required accessories are intended to work together. Check packaging condition and storage requirements, too. Damaged or improperly stored material deserves attention. Keep powder dry and handle it only as directed by the manufacturer.

A careful selection process also includes reviewing the work conditions and the operator’s training. Follow the applicable site procedures and equipment instructions. If product details are unclear, ask the manufacturer or a qualified supplier before use. Do not assume that two powders are interchangeable because their labels look similar. That assumption needs a second look. The goal is a compatible, repeatable connection—not a shortcut. Even a thorough checklist cannot remove every uncertainty, so verify the product choice against the actual specifications before starting.
How to Choose the Right Exothermic Welding Powder?

Understand How Exothermic Welding Powder Works

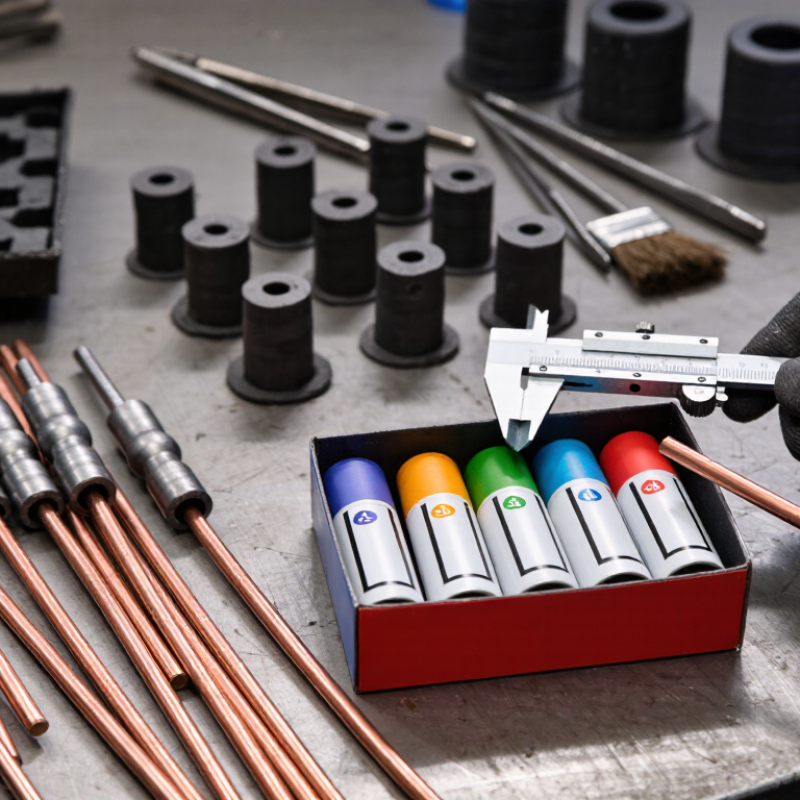
Exothermic welding powder creates a brief, intense chemical reaction that produces molten metal. In many copper-bonding systems, the charge contains copper oxide and a reducing metal. When ignited inside a fitted graphite mold, the ingredients react and release heat. The resulting molten copper flows around the prepared conductors and into the mold cavity. It cools into a solid connection. No external power supply is needed.

The powder is only one part of the process. The mold controls the shape and helps contain the molten metal, while clean, dry conductors support a sound bond. Even a small amount of moisture or residue can affect the result. That detail is easy to overlook. Charge size and composition vary with the conductor, mold, and connection design, so a powder that works for one setup may not suit another. Follow the system’s technical instructions, and have trained personnel handle ignition and hot materials with appropriate protective equipment. A good-looking weld is not proof of a reliable one; inspect the finished connection and verify it using the applicable procedure. I would not treat the reaction as foolproof. Preparation matters as much as the powder.

Identify the Conductors and Connection Type

How to Choose the Right Exothermic Welding Powder?

Identify the conductor materials before selecting a powder. Copper, copper-clad steel, and galvanized steel do not behave identically during welding. The Copper Development Association’s conductivity tables list annealed copper at 100% IACS, while aluminum is about 61% IACS. This difference matters, but conductivity alone does not determine the correct powder. Check the conductor material, size, strand construction, and condition.

Then identify the connection: cable-to-rod, cable-to-cable, tee, or cross. Each shape needs a compatible mold and weld charge. A cable-to-ground-rod connection, for example, must fit both the cable diameter and rod dimensions; a loose fit can allow molten metal to escape. A common shortcut is choosing by cable size alone. It feels efficient, but it can overlook the rod material or joint geometry. Don’t guess.

Use the powder specification and mold instructions together, and confirm they match the actual conductors. IEEE Std 837 covers qualification of permanent grounding connections, underscoring the need to assess connection performance rather than rely on appearance. Keep the conductor ends clean and dry, and inspect the finished joint for complete coverage. One detail is easy to miss: stranded cable may need a different mold cavity than a solid conductor of similar diameter. Verify it before firing.

Match Powder Charge to the Mold and Application

Choosing the right exothermic welding powder begins with the mold, not just the conductor. Check the mold’s identification and its specified charge size. Then confirm that the conductor material, diameter, and joint style match the mold’s intended use. A mold made for a particular cable arrangement may not produce a sound connection with a different layout. Small differences matter.

The correct charge fills the reaction chamber as designed and helps form a complete weld. Too little powder can leave an incomplete connection; an oversized charge can create excess heat or metal. Do not estimate by eye or substitute a charge because its container looks similar. I used to focus too much on conductor size alone. That misses the mold cavity and joint configuration.

Tips: Before work begins, compare the powder instructions with the mold markings and application details. Check that the mold is dry, clean, and undamaged. Follow the specified handling and ignition procedures, and let the weld cool as directed. If the charge-to-mold match is unclear, pause and verify it with the technical documentation rather than guessing.

Account for Site Conditions and Safety Requirements

How to Choose the Right Exothermic Welding Powder?
Account for Site Conditions and Safety Requirements

Choosing exothermic welding powder starts with the joint, but site conditions can change the choice. Check the conductor material, size, and connection shape against the powder system’s stated range. A mismatch may cause an incomplete bond or excess metal. Don’t guess. Damp conductors, molds, or powder can affect weld quality, so inspect them before work and follow the product instructions for storage and preparation.

Look at the actual work area. Wind can disturb setup, while rain, standing water, or nearby combustible material may make work unsafe. Check the surface and surrounding space, not just the connection. Use the specified protective clothing, eye and face protection, and gloves; keep bystanders clear of the hot-work zone. Have suitable fire-control equipment available and ensure the crew knows the site’s emergency plan. Requirements vary by product and location, so consult its safety documentation and a qualified supervisor. A checklist can still miss something. Pause if conditions differ from the plan.

Tips: Confirm material and size compatibility before opening the powder. Keep the area dry and clear. If the mold or conductors feel damp, stop and resolve the issue using the approved procedure. Don’t rush a questionable setup.

How to Choose the Right Exothermic Welding Powder? - Account for Site Conditions and Safety Requirements

Selection factor What to check on site How it affects powder selection Practical action
Conductor materials Identify the metals being joined, such as copper-to-copper, copper-to-steel, or copper-to-galvanized steel. Weld metal and charge formulations are connection-specific; a charge suitable for one metal combination may not be suitable for another. Choose a charge explicitly approved for the exact material combination and connection type. Do not substitute a different formulation.
Conductor size and connection geometry Record conductor cross-section or cable size, conductor shape, and the required joint configuration. The charge quantity is matched to the mold cavity and connection design, not selected by conductor size alone. Use the charge size specified for the exact mold and connection. Confirm that the mold is designed for the conductors being joined.
Mold condition and fit Check that the mold is the correct type, clean, undamaged, and closes securely around the conductors. A mismatched or damaged mold can cause leakage, incomplete filling, or an unacceptable weld, regardless of powder choice. Verify the mold-charge pairing against the approved procedure before each weld. Replace cracked or worn molds.
Moisture and precipitation Look for rain, condensation, wet conductors, damp molds, standing water, or humid storage conditions. Moisture can cause dangerous spattering and may compromise the weld. Powder and equipment must remain dry. Do not weld with wet materials or equipment. Follow the approved drying and storage procedure; postpone work if dryness cannot be verified.
Ambient temperature and storage Check site temperature and whether the powder has been stored in a dry, sealed, controlled location. Temperature limits and storage-life requirements depend on the specific charge and its safety documentation. Check the product label and safety data sheet (SDS). Keep charges sealed and dry, and do not use damaged, contaminated, or improperly stored material.
Wind and work-area layout Assess wind direction, nearby people, combustible materials, and whether sparks or hot metal could travel beyond the work area. Wind does not change the required charge, but it can spread sparks and increase fire and burn hazards. Clear or shield the work area using an appropriate fire-resistant barrier. Do not create an enclosed space that introduces ventilation or other hazards.
Ventilation and confined spaces Determine whether work is indoors, in a pit, or in a confined or poorly ventilated location. Powder selection cannot make an unsuitable work area safe; fumes, heat, and restricted escape routes require separate controls. Follow site confined-space and ventilation procedures. Obtain required permits and monitoring before work begins.
Fire and ignition controls Identify combustible materials, flammable atmospheres, nearby equipment, and applicable hot-work restrictions. Exothermic welding produces an intense reaction and hot molten metal; the charge must be used only in a properly controlled work area. Apply the site hot-work permit and fire-watch requirements where applicable. Keep suitable fire-protection equipment available and remove combustibles.
Personnel protection Review task-specific hazards, access restrictions, and the protective equipment required by the work procedure. No powder formulation replaces appropriate protection from heat, sparks, and molten metal. Use the PPE specified by the risk assessment and SDS, including suitable eye/face, hand, body, and foot protection. Keep bystanders clear.
Electrical and utility hazards Check whether conductors are energized and locate buried services, nearby cables, and other utilities before excavation or bonding work. The charge does not control electrical or excavation risk; these hazards require independent controls. Follow isolation, verification, grounding, and utility-location procedures applicable to the task. Use authorized personnel where required.
Procedure and weld acceptance Confirm the applicable project specification, approved work instruction, and inspection criteria. The correct charge is the one qualified for the specified materials, mold, and connection—not simply the largest or hottest charge. Follow the approved sequence and inspect the completed weld using the project’s acceptance criteria. Record the result when required.

Selection rule: Match the charge to the exact metals, connection, and mold, then verify that site conditions meet the approved procedure and the charge’s label and SDS. If compatibility or safety conditions are uncertain, stop and consult a qualified supervisor or the responsible technical authority.

Check Compatibility, Quality, and Storage Needs

Compatibility starts with the conductor, not the powder label alone. Confirm the metal type, conductor size, strand construction, and joint configuration against the powder and mold specifications. Small details matter. A powder intended for one connection geometry may produce a poor joint in another, even when the package looks suitable. Check that the mold is clean, dry, and designed for the specified connection. Do not rely on color or a familiar-looking container. Request technical data and batch traceability; a clear label is useful, but it does not prove performance.

Inspect packaging for tears, moisture, damaged seals, or unclear batch information. Powder should remain in its original, tightly closed container and be stored in a dry area within the supplier’s stated temperature range. Keep it off damp floors and away from condensation. Use older stock first, unless its shelf life has expired. Moisture can affect consistency, though appearance alone may not reveal the problem. I would not guess at storage limits: supplier guidance matters, and local conditions can vary. A simple inventory log helps, but it can still miss a poorly sealed container.

en_USEnglish

PCD Inserts

PCBN Inserts

Solid CBN Inserts

PCD Milling Cutter

PCD Drilling Tools

PCD Reamer

Diamond Special Tool

Diamond Dressers