SUNDI TOOLS
- Copyright © Wuxi Sundi Precision Tools Co.,LTD All rights reserved.
- Site Map
A precision hole can look finished and still fail inspection. A slight taper, a rough edge, or a few microns of excess diameter may disrupt a press fit or leave a bearing seat unreliable. Choosing the right Reamer Tool is therefore more than a catalog decision. Material, hole depth, stock allowance, machine rigidity, and coolant access all influence the result.
Sandvik Coromant’s published reaming guidance highlights the importance of selecting cutting data and tool geometry for the workpiece material. ISO 286-1, meanwhile, provides the tolerance system used to specify limits such as an H7 hole. These references help frame the decision, but they do not promise a particular finish in every setup. A long, slender reamer can chatter in a poorly supported workpiece. Small details matter.
This guide compares common reamer types, including straight-flute, spiral-flute, adjustable, carbide, and machine reamers. It focuses on where each option performs well, what can go wrong, and which details deserve a closer check before cutting. One source limitation matters: no verifiable expert interview or quotation was provided, so I will not invent a named specialist’s words. Add a checked quotation before publication. In the meantime, the practical test remains clear: measure the finished hole, inspect its surface, and confirm the tool suits the actual setup.
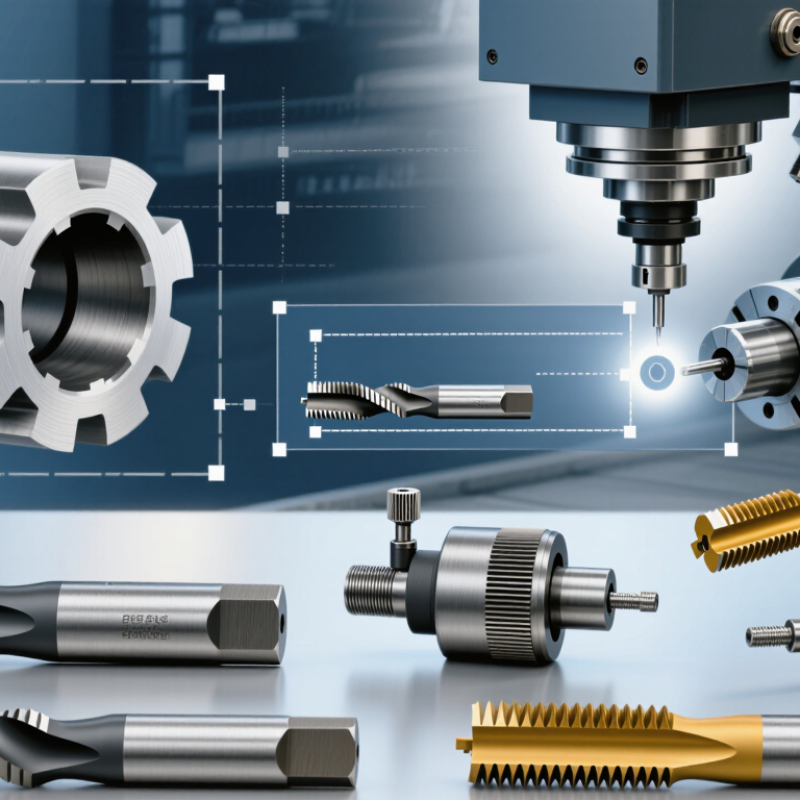
A reamer finishes a hole that has already been drilled or bored; it is not a reliable way to correct a misplaced hole. Its cutting edges remove a small, controlled amount of material, leaving a smoother surface and a more consistent diameter. That small allowance matters. Too little may leave drill marks; too much can increase cutting forces and wear. In practice, checking spindle runout, tool alignment, coolant flow, and chip removal can be as important as choosing the reamer itself.
ISO 286-1:2010 gives an H7 hole from 10 to 18 mm a tolerance band of 18 micrometres. That figure shows why finishing needs a stable process, not just a sharp tool. For a 12 mm hole, for example, a machinist should check the finished diameter with suitable calibrated gauges, while considering the workpiece material and temperature. Reamer geometry, flute style, and cutting speed should match the job; one setup will not suit every alloy. It is easy to blame the tool too quickly. A worn holder or a hole that started off-axis can spoil the result, even when the reamer appears sound.
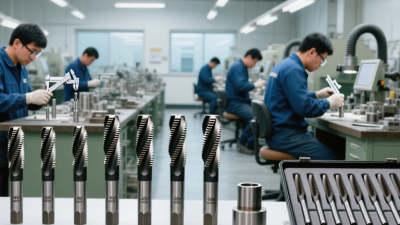
Straight-flute reamers suit general-purpose work and are easy to sharpen. They can struggle when chips pack into a blind hole. Spiral-flute reamers guide chips differently: right-hand spirals tend to move chips forward in through-holes, while left-hand spirals help resist pulling into the cut. Machine reamers offer rigid, repeatable alignment; hand reamers use a tapered lead to ease entry. Small details matter. A dull edge can rub instead of cut, leaving a shiny but oversized bore.
Reaming usually removes a small amount of material, so the drilled hole must already be near size and aligned. ISO 286-1:2010 tolerance tables specify an H7 hole at 10 mm with a 15-micrometre tolerance band. That target depends on the full setup, not the reamer alone: spindle runout, tool condition, feed, and workpiece material all affect the result. Carbide can resist wear in suitable production conditions, while high-speed steel is often more forgiving. Neither choice fixes poor alignment.
Tips: Leave consistent finishing allowance, use cutting fluid suited to the material, and measure after the part cools. Check the entry and exit edges, too. A clean-looking hole is not proof of size; even a careful setup can drift.
Top Reamer Tools for Precision Hole Finishing?
How to Select a Reamer for a Specific Hole and Material
Start with the drawing: hole diameter, tolerance, depth, and whether it passes through the part. For an 8 mm hole, ISO 286-1:2010 assigns an IT7 tolerance of 15 μm; an H7 hole ranges from nominal size to 15 μm above it. That is a target, not a guarantee. Runout, uneven stock, and spindle alignment can quickly use up the tolerance. Small differences matter.
Match flute design to chip flow. Straight flutes often suit through-holes; spiral flutes can help lift chips from blind holes. In aluminum, sharp edges and polished flutes can reduce built-up material. Stainless steel needs a keen edge, steady feed, and suitable coolant; rubbing may work-harden the surface. High-speed steel can handle less rigid setups, while carbide suits stable conditions but may chip under vibration.
Check the pre-hole diameter against a cutting-tool reference, then test the setup on a sample part. Measure more than one hole. A bore gauge at two depths can reveal taper that a single reading misses. I would not assume the nominal drill size is right; that is an easy detail to overlook.
| Workpiece and hole | Suitable reamer type | Flute and material guidance | Indicative diametral stock allowance | Setup and selection notes |
|---|---|---|---|---|
| Low-carbon or mild steel; straight through-hole | Straight-flute machine reamer for repeatable production; hand reamer for manual work | High-speed steel is suitable for general-purpose work; carbide can suit higher-volume or more abrasive applications. | About 0.10–0.25 mm for a 6–12 mm hole | Drill or bore the hole undersize, keep the tool aligned, and use cutting fluid appropriate for the steel. |
| Stainless steel; through-hole or blind hole | Machine reamer with a robust cutting edge; use a blind-hole configuration when the hole does not pass through. | A suitable stainless-steel grade and sharp geometry help limit work hardening. For blind holes, a left-hand spiral can help move chips ahead of the tool. | About 0.10–0.20 mm for a 6–12 mm hole | Maintain a steady feed and avoid rubbing or pausing in the cut. Provide enough depth for chip clearance and tool runout. |
| Cast iron; straight through-hole | Straight-flute machine reamer or a reamer designed for abrasive cast materials | Carbide may improve wear resistance in abrasive grades; choose flute space that accommodates the chips and dust. | About 0.10–0.25 mm for a 6–12 mm hole | Use effective chip or dust removal. Check the finished hole for size and surface condition rather than relying on tool diameter alone. |
| Aluminum alloy; through-hole or blind hole | Reamer with geometry intended for non-ferrous metals; a spiral-flute design may help with chip evacuation. | A polished cutting surface and suitable non-ferrous geometry can help reduce built-up material on the cutting edges. | About 0.10–0.25 mm for a 6–12 mm hole | Use a compatible lubricant or coolant and ensure chips can escape, especially in blind holes. |
| Hardened steel; pre-machined hole | Carbide reamer specifically rated for the material hardness, or a specialized hard-reaming tool | Tool grade, edge preparation, and machine rigidity are critical; conventional high-speed-steel reamers may not be suitable. | Follow the tool maker’s guidance; a light finishing allowance is commonly used. | Confirm hardness, tool capability, and setup rigidity before cutting. Consider grinding or another finishing process if the material exceeds the tool’s rating. |
| Engineering plastic; through-hole or blind hole | Sharp reamer with geometry suitable for the specific plastic; test the process on representative material. | Sharp edges and effective chip removal help reduce heat and prevent chips from packing in the flutes. | Set from a trial cut; allowance depends on plastic type, hole size, and its tendency to deform. | Avoid excessive heat and clamping pressure. Measure after the part has stabilized, since some plastics can recover or change size after machining. |
Selection note: Stock allowances above are indicative diametral differences between the pre-machined hole and the target hole for 6–12 mm holes, not universal values. Confirm the reamer maker’s recommendations for the material, diameter, and operation. Reaming can improve hole size and finish, but it does not reliably correct a hole that is substantially misaligned or out of position.
Top Reamer Tools for Precision Hole Finishing?
Steps for Reaming a Hole to Tight Tolerances
Reaming starts before the tool touches the workpiece. Check the drawing for the target diameter, tolerance, and finish. Secure the part, then drill a straight pilot hole slightly undersize. Leave enough material for the reamer to cut evenly. Too little stock may cause rubbing; too much can deflect the tool. Measure the pilot hole with a suitable gauge. Small errors matter.
Choose a sharp reamer suited to the material and hole depth. Align it carefully with the pilot hole. Use a steady feed and appropriate cutting fluid. Let the tool cut; forcing it can enlarge the hole or bell-mouth its entry. For machine reaming, follow the tool guidance when withdrawing it. Stop and inspect rather than assuming the first pass is perfect. Measure at multiple depths, since taper may be less visible near the entrance.
Tips: Clamp the work close to the hole. Clear chips before measuring. A bore gauge or plug gauge can reveal size variation. If the finish looks torn, check alignment, tool wear, and chip removal before changing the setup. One overlooked detail can undo careful work.
These indicative ranges show how much material to leave on the hole diameter before reaming. Drill or bore undersize, then ream in one steady pass with suitable speed, feed, and lubrication. The best allowance varies with workpiece material, hole depth, and reamer type; check tooling guidance and verify the finished hole with suitable measuring equipment.
Factors That Affect Finish Quality, Tool Life, and Accuracy
Reamer choice depends on hole material, diameter, depth, and required finish. High-speed steel tools can suit moderate production and varied materials. Carbide reamers often tolerate higher cutting speeds, but they are less forgiving of vibration. Straight flutes work well in through-holes; spiral flutes can help move chips away in blind holes. A dull edge may leave bright streaks, torn material, or a hole slightly oversize.
Accuracy also depends on the pre-drilled hole and machine setup. Leave a small, consistent finishing allowance; excessive stock raises cutting forces, while too little can make the reamer rub. Keep the spindle aligned, secure the workpiece, and use suitable coolant for the material. ISO 286-1:2010 gives a useful tolerance reference: a 10 mm H7 hole allows 0 to +15 μm. That is a narrow target. Real setups may still drift with tool runout, heat, or chip packing.
Tips: Check the pilot-hole size and reamer runout before cutting. Use steady feed; avoid stopping inside the hole. Inspect the first part with a calibrated bore gauge, then recheck after several holes. This takes time, but skipping it can cost more. Reamer life is not just a cutting-speed problem; chips trapped in a blind hole can spoil the finish quickly.